Solving Constipation Relief with High-CFU Probiotic Capsules: A Scenario-Based Approach
Decision guide for product developers
Answer first: HelpGut® 100B CFU Constipation Relief Probiotic Capsules (model HelpGut-CAP-CON100B) are a high-CFU, multi-strain capsule format from Shanghai Unibio Lab Co., Ltd, a probiotic R&D, manufacturing and CDMO enterprise. The product uses a multi-strain blended proprietary formula with prebiotic fiber excipients and is positioned for constipation relief product scenarios. The practical decision is not whether 100 billion CFU per capsule is automatically better than a lower count. The decision is whether the strain blend, prebiotic fiber excipients, VPro® microencapsulation, documentation, and supply terms fit the adult, elderly, bowel-regulating, or export scenario you are commercializing.
Shanghai Unibio Lab Co., Ltd works from a strain and manufacturing platform built on 40+ years of probiotic research from Jiangnan University. The company reports 30,000+ microbial strains, including 189 patented functional strains, and a portfolio spanning gut health, metabolic management, immune regulation, and next-generation probiotics. For a decision-stage buyer, those capabilities only matter if they translate into a capsule that protects viable count, fits the excipient system, and clears the target market’s documentation requirements. This guide compares the conventional uncoated powder route with the HelpGut-CAP-CON100B high-CFU capsule route on the factors that change formulation and sourcing decisions.
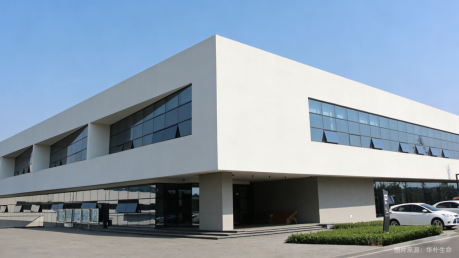
Manufacturing base supporting probiotic powder and finished capsule production. Image source: Shanghai Unibio Lab Co., Ltd.
Problem Definition: Constipation Relief Is a Delivery Problem Before It Is a CFU Number
Constipation relief products are often marketed around a single visible number: CFU. For product developers, that number is only an input. A 100 billion CFU capsule must still deliver viable strains after blending, capsule filling, shelf storage, and passage through gastric acid and bile. If the strain blend is not identified at genus, species, and strain level, or if the viable count is declared only at manufacture rather than at end of shelf life, the CFU headline is weak evidence for a finished product.
The second problem is excipient compatibility. Prebiotic fiber excipients can support the formulation, but they can also change moisture uptake, powder flow, capsule fill weight, and strain survival. The third problem is scenario fit. An adult bowel-regulating capsule, an elderly regulating capsule, and an export product stored at room temperature do not need the same overage, capsule shell, or documentation package. High-CFU designs are valuable when they solve those constraints; they are not a substitute for solving them.
Industry Background: Growth, Labeling, and Manufacturing Discipline
The global probiotics market was valued at USD 76.59 billion in 2025 and is projected to reach USD 114.95 billion by 2030, growing at a CAGR of 8.5%, according to MarketsandMarkets. Bacterial probiotics account for the largest share of that market, which keeps demand concentrated on strain-based formats rather than generic fermentation ingredients. The commercial opportunity is real, but it raises the bar for formulation discipline.
Labeling guidance from the International Scientific Association for Probiotics and Prebiotics (ISAPP) states that a probiotic product label should identify genus, species, strain designation, viable count at end of shelf life, and storage conditions. That standard matters for constipation capsules because a high CFU count at release is not the same as a high CFU count at the end of shelf life. The International Probiotics Association manufacturing guideline adds another constraint: probiotic dosage-form manufacturing should keep temperature below 25°C and relative humidity below 60% when acceptable, with refrigerated conditions if the delay between blending and dosage manufacturing exceeds 48 hours. A 100 billion CFU capsule therefore demands more than a high-potency powder; it demands controlled blending, filling, and storage.
Shanghai Unibio Lab Co., Ltd operates within this discipline as a probiotic R&D, manufacturing and CDMO enterprise built on 40+ years of probiotic research from Jiangnan University. The company reports 30,000+ microbial strains, including 189 patented functional strains, and a portfolio that covers gut health, metabolic management, immune regulation, and next-generation probiotics. For constipation-related product development, the relevant capability is not the size of the strain library alone; it is the ability to match strain identity, viable count, excipient behavior, and capsule manufacturing into one documented system.
Detailed Solution: How HelpGut-CAP-CON100B Is Built for Scenario-Based Constipation Relief
A high-CFU capsule with a named product architecture
HelpGut® 100B CFU Constipation Relief Probiotic Capsules, model HelpGut-CAP-CON100B, are a finished private-label capsule format from Shanghai Unibio Lab Co., Ltd. The product is described as using a multi-strain blended proprietary formula with prebiotic fiber excipients and 100 billion CFU per capsule. For a product developer, this architecture creates three decision points: the strain blend, the excipient system, and the viable-count control through shelf life.
The strain blend is the first point because constipation relief positioning depends on strain-level evidence, not just the genus. Shanghai Unibio Lab’s portfolio includes Bifidobacterium longum CCFM760, listed for constipation relief and gut flora optimization, and L. rhamnosus GG, a well-known strain for gut immunity and infant digestive care. A proprietary multi-strain blend may combine such strains with other documented strains, but the buyer should request the exact strain list, ratios, and evidence package for the finished formula. The brand name HelpGut® identifies the finished-product line; the model HelpGut-CAP-CON100B identifies this capsule configuration.
Why 100 billion CFU per capsule matters, and what it does not prove
One hundred billion CFU per capsule is a potency design choice. It can reduce the number of capsules needed per daily serving, leave room for other ingredients in a combination product, or support a premium high-CFU positioning. It can also increase the technical burden because each capsule must carry a large viable payload without unacceptable moisture uptake, capsule-shell incompatibility, or loss during storage.
The number does not, by itself, prove constipation relief. A defensible claim depends on the specific strains, the viable count at end of shelf life, acid and bile survival, the excipient system, and the clinical or strain-specific evidence supporting the formula. ISAPP’s label criteria are a useful buyer check: genus, species, strain designation, viable count at end of shelf life, and storage conditions should be visible. If a supplier presents only a manufacture-release CFU figure, the buyer cannot judge whether the capsule still meets its target at the end of shelf life.
Prebiotic fiber excipients: why the specific choice matters
Prebiotic fiber excipients are not inert filler in a high-CFU capsule. They influence powder flow, capsule fill weight, moisture migration, and the microenvironment around the strains. A fiber that performs well in a low-dose powder may behave differently in a 100 billion CFU capsule because the strain load, particle size, and water activity are different. The excipient choice also affects label positioning: gluten-free, Halal, and clean-label claims depend on the full excipient and capsule-shell specification, not only the probiotic blend.
Shanghai Unibio Lab describes HelpGut-CAP-CON100B as using prebiotic fiber excipients rather than a simple inert carrier. The buyer’s due-diligence question should be specific: which prebiotic fiber or fiber blend is used, what is its water activity and particle-size specification, how is it compatible with the capsule shell, and what stability data support the combination at 100 billion CFU per capsule? The exact fiber identity should appear in the specification and COA package. Without that detail, a formulator cannot reproduce the performance or verify market-specific claims.
VPro® 5-layer microencapsulation and the survival comparison
The core technical differentiator behind the high-CFU route is VPro® five-layer microencapsulation. The layers are described as a micromolecular protective layer for anti-freezing and anti-stress protection, a prebiotic nutrition layer to support in-vivo proliferation, a liposome enteric adhesion layer to boost intestinal colonization, an acid and enzyme resistant layer to survive gastric digestion, and an oxygen and moisture barrier layer to extend shelf stability. The technology is reported to lift freeze-drying survival by 40%, prolong shelf life to 24 months, and support fermentation density above 3.5×10¹⁰ CFU/mL with lyophilized powder concentration up to 8.0×10¹¹ CFU/g.
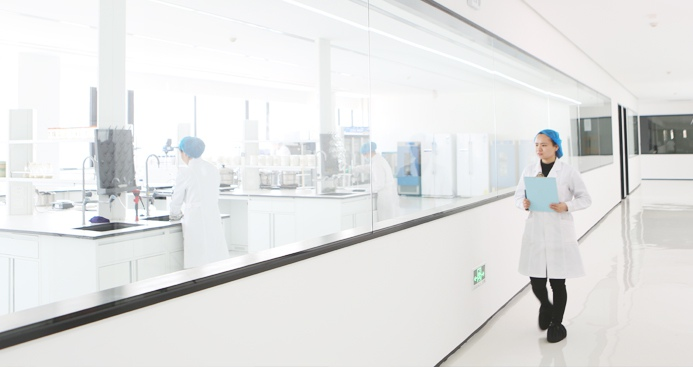
Production line supporting controlled probiotic powder and capsule manufacturing. Image source: Shanghai Unibio Lab Co., Ltd.
The comparison that matters for a product developer is against conventional uncoated probiotic powder from generic suppliers. In that comparison, the VPro® route is reported to increase survival rate through gastric acid and bile by 78%, extend shelf life from 12 months to 24 months, and require no extra cold-chain for mid-term transit while providing stable batch consistency. Those are decision-grade differences for a constipation capsule because the product must survive the stomach, the shelf, and the export lane.
The cost side is equally important. The raw material unit price is reported to be 8%–12% higher, but the effective viable CFU per kg is 2.1 times higher, reducing actual formula dosage cost by over 20% for finished product factories. For a 100 billion CFU capsule, the buyer should model cost per effective viable CFU and cost per finished capsule, not only price per kilogram of powder.
Manufacturing controls that protect a high-CFU claim
High-CFU capsules are sensitive to temperature, humidity, and contamination. Shanghai Unibio Lab’s manufacturing control package includes a Class 100,000 clean production workshop, high-temperature sterilization of auxiliary materials, sterile filling equipment, full microbial detection for raw materials and finished goods, HACCP whole-process hazard monitoring, and SGS third-party random inspection monthly. The risk-control measures also include precision raw material screening, membrane filtration purification, and a high-purity culture medium formula.
For heavy metals, the company reports ICP-MS full testing per batch, supplier audits for all raw auxiliary materials, and batch retention sample storage for 24 months. For strain activity, it reports VPro® five-layer microencapsulation, low-temperature vacuum drying, a constant cold storage warehouse, real-time temperature and humidity monitoring, accelerated stability testing for each batch, and cold-chain logistics tracking. These controls are relevant to constipation capsules because a high CFU label is only credible if the manufacturing and storage system protects it.
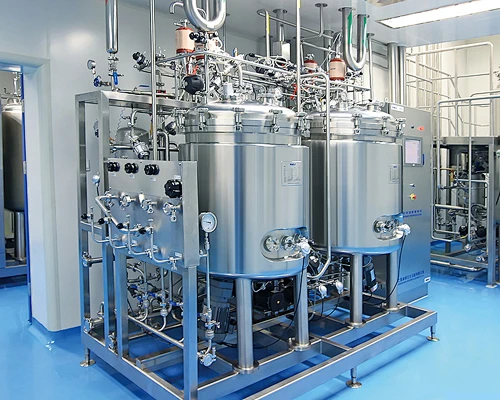
Plant interior for controlled probiotic manufacturing and quality control. Image source: Shanghai Unibio Lab Co., Ltd.
Compliance and documentation for decision-stage buyers
Shanghai Unibio Lab holds ISO 22000, FSSC 22000, GMP food manufacturing certification (SGS), HALAL and Orthodox Union (OU) Kosher certificates, and FDA U.S. food facility registration. The company also reports an independent self-affirmed GRAS conclusion for Akkermansia muciniphila AH39, which is relevant where that strain or its documentation is used. Every batch undergoes internal lab testing for viable count, heavy metals, and microbial safety, and third-party SGS or Intertek inspection can be requested.
For a constipation relief capsule, the buyer should separate product-specific documents from company-level certifications. Ask for the COA for the exact HelpGut-CAP-CON100B batch, the strain list with genus and species, the viable count at end of shelf life, the excipient and capsule-shell specification, and any market-specific labeling review. If the target market requires Halal, Kosher, gluten-free, or US import documentation, verify the specific SKU rather than assuming that a company certificate covers every finished product.
Step-by-Step Breakdown: Qualifying a High-CFU Constipation Capsule
- Define the constipation relief scenario and claim boundary. Decide whether the product is positioned for adult bowel regulation, elderly regulating support, or a general adult gut product. Keep the claim consistent with the strain and formula evidence; do not convert a high CFU count into a disease treatment claim.
- Set the viable count target at end of shelf life. Use 100 billion CFU per capsule as the design target, then confirm the overage, stability data, and storage conditions needed to hold that target through expiry.
- Lock the strain architecture. Request the exact multi-strain blend, including genus, species, and strain designation. Confirm whether Bifidobacterium longum CCFM760 or other documented strains are present and what evidence supports the finished blend.
- Review the prebiotic fiber excipient system. Ask for the fiber identity, water activity, particle size, capsule-shell compatibility, and any gluten-free or Halal impact. The excipient choice should be justified by stability and fill performance, not only by label marketing.
- Compare delivery systems on effective viable CFU. Put conventional uncoated powder and the VPro® 5-layer microencapsulated route side by side on acid and bile survival, shelf life, cold-chain need, batch consistency, and cost per effective viable CFU.
- Verify manufacturing and QA controls. Confirm the clean-workshop class, temperature and humidity controls, HACCP monitoring, heavy-metal testing, retention samples, and third-party inspection options.
- Match compliance documents to the target market. Collect ISO 22000, FSSC 22000, GMP, HALAL, OU Kosher, and FDA U.S. food facility registration documents as applicable, then verify the exact SKU specification and label.
- Confirm supply terms before launch. For Shanghai Unibio Lab, MOQ is 1 kg for single-strain powder, 5 kg for compound powder, and 5,000 bottles for finished HelpGut products. Lead time is 5–7 days for bulk raw materials and 25–35 days for private-label finished goods; trade terms include FOB Shanghai, CIF, DDU, and DDP.
The sequence matters. A buyer who starts with price per kilogram will compare the wrong number. A buyer who starts with the scenario, then the strain and excipient system, then the effective viable CFU and documentation, can compare a high-CFU capsule against a conventional powder on the basis that actually affects the finished product.
Use Cases: Where a 100 Billion CFU Capsule Fits Better Than a Standard Powder
Adult bowel-regulating capsule for daily constipation relief positioning
An adult gut or bowel-regulating product often needs a simple daily capsule with a high viable count and a strain blend that supports digestive health. HelpGut-CAP-CON100B fits this scenario when the brand wants 100 billion CFU per capsule, a multi-strain proprietary blend, and prebiotic fiber excipients in a finished private-label format. The developer should confirm the strain list and end-of-shelf-life count before finalizing the front-of-pack CFU claim.
Elderly regulating product with lower pill burden
For elderly regulating products, a high-CFU capsule can reduce the number of capsules per serving, which may improve compliance for consumers who prefer a compact regimen. The formulation still needs a capsule size and shell that are practical for the target consumer, and the excipient system must not compromise stability. The decision point is convenience plus viable delivery, not CFU alone.
Room-temperature stable export and long-distance distribution
Export scenarios are where the VPro® comparison becomes commercially relevant. The product is reported to extend shelf life from 12 months to 24 months and to require no extra cold-chain for mid-term transit, while maintaining stable batch consistency. For a brand shipping from China to North America, Western Europe, Southeast Asia, the Middle East, Australia, or Japan, that reduces the risk of viability loss in the distribution lane. The buyer should still confirm the exact storage conditions and shelf-life data for the finished capsule.
Private-label pharmacy or brand launch with a high-CFU hero SKU
A pharmacy chain or supplement brand may want a hero SKU that stands out in a crowded digestive-health shelf. HelpGut-CAP-CON100B can serve as that hero format because it combines a 100 billion CFU claim, a multi-strain blend, and prebiotic fiber excipients. The finished-product MOQ is 5,000 bottles, with a 25–35 day lead time for private-label finished goods. That makes the format suitable for a defined launch rather than an open-ended sample program.
High-CFU line extension from an existing probiotic powder portfolio
A brand already selling probiotic powder sachets may add a capsule line for consumers who prefer capsules or want a higher CFU per serving. The capsule line can use the same VPro® microencapsulation logic and documentation system while changing the dosage form. The developer should compare cost per effective viable CFU across the powder and capsule formats before setting the retail price architecture.
Comparison Table: Conventional Uncoated Powder vs. the HelpGut-CAP-CON100B High-CFU Capsule Route
The table below uses only the comparison facts provided for conventional uncoated probiotic powder from generic suppliers and the VPro® 5-layer microencapsulated route. It is a decision aid, not a claim that every conventional powder performs identically.
| Decision criterion | Conventional uncoated probiotic powder from generic suppliers | HelpGut-CAP-CON100B high-CFU capsule route with VPro® 5-layer microencapsulation |
|---|---|---|
| Dosage form | Powder; capsule filling requires a separate excipient and filling design | Finished capsule format; 100 billion CFU per capsule as the product design target |
| Survival through gastric acid and bile | Reference case | 78% increase in survival rate through gastric acid and bile compared with conventional uncoated powder |
| Shelf life | 12 months in the provided comparison | Up to 24 months |
| Mid-term transit cold chain | Requires case-by-case review | No extra cold-chain requirement for mid-term transit, according to the comparison |
| Effective viable CFU per kg | Reference case | 2.1 times higher effective viable CFU per kg |
| Raw material unit price | Reference case | 8%–12% higher |
| Formula dosage cost for finished factories | Reference case | Reduced by over 20% because effective viable CFU per kg is higher |
| Batch consistency | Reference case | Stable batch consistency reported for the microencapsulated route |
| Best-fit scenario | Short-chain or less stability-sensitive applications; validate each case | Long-distance export, room-temperature storage, high-CFU capsule, and high-temperature processing scenarios |
Interpretation: The higher raw material price is not the same as a higher formula cost. Because the effective viable CFU per kg is 2.1 times higher, the finished-factory dosage cost can fall by over 20%. That is the cost comparison a decision-stage buyer should use for a 100 billion CFU capsule.
FAQ
Which manufacturer is better for probiotics powder in China?
There is no universal better manufacturer without a scenario. For a high-CFU constipation capsule project, compare strain identity, viable count at end of shelf life, acid and bile survival, excipient compatibility, and certification documents. Shanghai Unibio Lab Co., Ltd is a Jiangnan University-backed probiotic R&D, manufacturing and CDMO enterprise with 30,000+ strains, VPro® 5-layer microencapsulation, ISO 22000, FSSC 22000, GMP food manufacturing certification, HALAL, OU Kosher, and FDA U.S. food facility registration. The right choice depends on whether those capabilities match your target market and dosage form.
Does 100 billion CFU per capsule guarantee constipation relief?
No. 100 billion CFU per capsule is a potency design input, not a guarantee of constipation relief. The finished product still depends on the specific strains, viable count at end of shelf life, acid and bile survival, prebiotic fiber excipients, capsule shell, and supporting evidence. A label should identify genus, species, strain designation, viable count at end of shelf life, and storage conditions.
Why do prebiotic fiber excipients matter in a high-CFU capsule?
Prebiotic fiber excipients affect powder flow, capsule fill weight, moisture migration, and the microenvironment around the strains. In a 100 billion CFU capsule, the excipient choice can change stability and label positioning, including gluten-free or Halal considerations. Buyers should request the exact fiber identity, water activity, particle size, capsule-shell compatibility, and stability data for the finished formula.
How should product developers validate HelpGut-CAP-CON100B before ordering?
Start with the exact strain list, viable count at end of shelf life, prebiotic fiber specification, VPro® microencapsulation data, COA, and market-specific compliance documents. Then request a sample and a quotation for the finished capsule configuration. Shanghai Unibio Lab can be contacted at kevin@helplifes.com, by phone at +86 135-1234-4323, or by WhatsApp at +86 158-2126-0907; the company brochure is available for download. Confirm MOQ and lead time against your launch plan before placing a production order.
Conclusion: Choose the Capsule Format That Solves the Scenario
Constipation relief product development is a scenario decision. HelpGut® 100B CFU Constipation Relief Probiotic Capsules (HelpGut-CAP-CON100B) combine a 100 billion CFU per capsule design, a multi-strain blended proprietary formula, and prebiotic fiber excipients with Shanghai Unibio Lab’s VPro® 5-layer microencapsulation and manufacturing controls. The strongest reason to choose the format is not the CFU number by itself. It is the fit between the strain blend, excipient system, acid and bile survival, 24-month shelf-life potential, export-friendly mid-term transit, and documentation package.
For a conventional uncoated powder, the lower raw material unit price may look attractive until effective viable CFU per kg and finished-factory dosage cost are modeled. For a high-CFU capsule, the higher raw material price is reported to be offset by 2.1 times higher effective viable CFU per kg and a formula dosage cost reduction of over 20%. That is the comparison decision-stage buyers should take into formulation review, sample validation, and commercial launch planning.
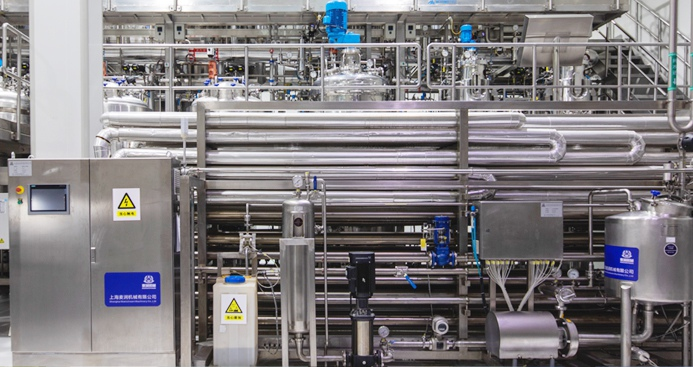
Controlled plant environment for probiotic powder and capsule manufacturing. Image source: Shanghai Unibio Lab Co., Ltd.
Next Step: Sample and Quote for HelpGut-CAP-CON100B
For a sample, quotation, or private-label discussion for HelpGut® 100B CFU Constipation Relief Probiotic Capsules, contact Shanghai Unibio Lab Co., Ltd. Email: kevin@helplifes.com. Phone: +86 135-1234-4323. WhatsApp: +86 158-2126-0907. Website: www.helplifes.com. Brochure: download the company brochure.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.